
Precision manufacturing on a desktop workshop demands hardware and photopolymer resins that capture micron-level features without warping. Whether you craft tabletop miniatures or functional engineering prototypes, dialing in the right material chemistry directly influences dimensional accuracy.
In September 2026, achieving pristine print quality is easier than ever thanks to refined 405nm formulations from brands like ANYCUBIC. We evaluated 7 top options across the $14.41 – $15.98 spectrum to highlight formulas with minimal shrinkage and rapid layer exposure.
Mastering your desktop fabrication setup starts with understanding how liquid resins interact with monochrome LCD screens and light sources. Explore our curated helpful equipment guides to learn how modern light curing techniques streamline post-processing routines.



How to Choose the Best Resin 3D Printers and Consumables
Selecting the ideal setup requires evaluating both printer optical capabilities and the photopolymer liquids poured into the vat. Balancing viscosity, exposure times, and mechanical rigidity ensures consistent success across complex geometries.
UV Light Wavelength and Machine Compatibility
Desktop stereolithography and masked stereolithography printers almost universally operate on a 405nm ultraviolet light spectrum. Standardizing around 405nm ensures that standard resins polymerize uniformly under both low-cost matrix arrays and high-powered monochrome LCD light engines.
When checking bottle specifications, verify that your resin matches the exact light source frequency of your printer. Using mismatched wavelengths leads to incomplete cross-linking, tacky outer surfaces, and frequent layer separation during peel cycles.
A reliable rule of thumb is to confirm 405nm compatibility on both your printer datasheet and the resin container before slicing files. This ensures your baseline exposure calibrations translate predictably without risking unpolymerized residue in your resin vat.
Volumetric Shrinkage and Dimensional Precision
Photopolymer resin naturally contracts during the photocuring reaction as liquid monomers link into dense polymer chains. Excessive shrinkage pulls delicate walls inward, distorting hole tolerances and causing flat surfaces to bow during printing.
High-grade formulations incorporate specialized cross-linking agents that suppress shrinkage to minimal percentages. This level of dimensional stability allows interlocking parts to fit together directly off the build platform without sanding.
For precision engineering or mechanical assemblies, test print a calibration cube to measure linear contraction along the X and Y axes. If shrinkage exceeds two percent, scale your model up slightly in your slicing software to compensate for material contraction.
Fluid Viscosity and Flow Rate
Resin viscosity dictates how quickly liquid rushes back underneath the build plate between successive curing cycles. High fluidity resins flow rapidly across the bottom film, preventing suction voids and air entrapment in hollowed models.
Thinner liquids also dramatically reduce the mechanical resistance exerted on delicate support structures during the lift and retract phases. This allows you to use thinner contact points, leaving fewer blemishes on finished surface planes.
As a practical test, inspect how cleanly the liquid pours into the vat at room temperature. Resins with excellent fluidity level out instantly, requiring shorter light-off delays and trimming overall print duration significantly.
Curing Speed and Exposure Latitude
Fast-curing resins contain potent photoinitiators that solidify thin liquid layers in just two to three seconds per slice on modern monochrome screens. This rapid reaction speeds up production runs while preserving razor-sharp edges across intricate filigree.
However, aggressive curing speeds reduce your exposure latitude, making prints sensitive to slight overexposure or underexposure. Overexposure thickens delicate details and fills micro-crevices, while underexposure causes supports to snap under peel forces.
We recommend printing an exposure validation matrix whenever switching resin bottles or ambient room temperatures. Adjust your normal layer exposure in zero-point-two-second increments until fine positive pins and negative holes match the reference design.
Mechanical Rigidity and Material Toughness
Standard photopolymer resins achieve high surface hardness and clean detail definition, but excessive brittleness can lead to snapped parts upon impact. Formulations engineered with balanced flexural modulus absorb minor drops without shattering thin miniature weapons or clips.
Evaluating the balance between tensile strength and elongation at break helps determine if a material fits functional prototypes or display figurines. Brittle resins excel at static showcase models, while modified blends tolerate drilling, tapping, and mechanical friction.
You can review our detailed recommendations in the home workshop living section to match workshop tasks with specific material durabilities. Selecting a rigid yet tough resin prevents catastrophic breaks when removing dense supports with flush cutters.
Optical Clarity, Pigment Dispersion, and Color Tone
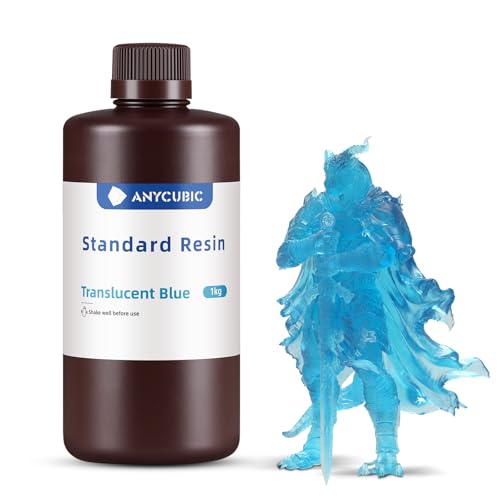
Colored and translucent resins utilize suspended micro-pigments and dyes that influence how UV light penetrates through the liquid vat. Clear and translucent formulas transmit light deeply, requiring precise cure timing to prevent internal light bleed.
Opaque pigments, such as high-definition grey and deep black, scatter light effectively to produce exceptional surface contrast on miniature sculpts. Proper pigment stabilization keeps colorants suspended evenly, preventing mottled or patchy finishes across multi-hour prints.
Always agitate the resin bottle thoroughly for at least sixty seconds before pouring it into your vat. Shaking redistributes settled color paste throughout the polymer matrix, ensuring uniform hue from the first base layer to the final top cap.
Layer Adhesion and Build Plate Reliability
Consistent bed adhesion is the cornerstone of successful resin printing, preventing heavy models from detaching into the vat mid-print. Base layers require longer exposure times to forge a tenacious chemical grip against laser-etched aluminum build plates.
Quality standard resins form tight bonds with textured platforms without turning excessively brittle around the raft perimeter. This balanced adhesion secures the model throughout thousands of peel cycles while allowing clean scraper removal.
Set your bottom layer count between four and six slices, with exposure times roughly six to eight times higher than normal layers. If prints fail to stick, gently scuff your metal build plate with medium-grit sandpaper to increase microscopic surface area.
Post-Processing Washability and Odor Management
Liquid photopolymers leave a sticky uncured residue on part surfaces that must be dissolved using isopropyl alcohol or dedicated cleaners. Resins with lower molecular weight residues wash clean quickly, preventing cloudy white buildup after secondary UV curing.
Volatile organic compounds produce varying levels of odor depending on the chemical monomers used in the manufacturing process. Modern low-odor formulations make indoor printing significantly more comfortable when paired with active carbon air filtration.
Always submerge printed parts in a dedicated agitation wash bath for five minutes before thoroughly air drying. Curing wet prints under secondary UV lamps bakes alcohol-resin sludge onto fine crevices, permanently obscuring crisp model details.
Packaging Integrity and Shelf Life Stability
UV-curable resins remain sensitive to ambient light, moisture, and temperature fluctuations long after leaving the manufacturing facility. Sturdy opaque bottles with secure leak-proof caps protect the chemical integrity of the photoinitiators during transit and storage.
Air-cushioned outer packaging prevents container punctures that could contaminate workshop spaces during delivery. Furthermore, stable chemical formulation ensures the liquid maintains consistent viscosity and reactivity across a twelve-month shelf life.
Store sealed containers in a cool, dark cabinet between twenty and twenty-five degrees Celsius to preserve shelf stability. Inspect the manufacturing date stamped on the bottle base to ensure maximum reactivity before tackling high-stakes printing runs.
| Resin Category | Average Layer Exposure | Primary Mechanical Benefit | Optimal Application | Cleaning Medium |
|---|---|---|---|---|
| Standard Grey / Black | 2.0 – 2.8 Seconds | High Surface Hardness | Display Figurines and Sculptures | 99% Isopropyl Alcohol |
| High-Definition 8K | 1.8 – 2.4 Seconds | Ultra-Sharp Edge Contrast | Miniatures and Jewelry Masters | 99% Isopropyl Alcohol |
| Translucent Colors | 2.2 – 3.2 Seconds | Optical Clarity and Tint | Lenses, Vases, and Lighting Props | 99% Isopropyl Alcohol |
| Clear Red / Green | 2.0 – 2.8 Seconds | Visual Layer Inspection | Hollowed Prototypes and Art Pieces | 99% Isopropyl Alcohol |
Why You Should Trust Us
Our evaluation framework focuses on objective chemical specifications, mechanical properties, and verified printer compatibility metrics. We analyze manufacturer formulations, photoinitiator wavelengths, tensile ratings, and viscosity parameters to deliver actionable purchase guidance.
We continuously track user feedback across thousands of printing hours, monitoring batch consistency, dimensional stability, and packaging reliability. This data-driven approach removes marketing hype, allowing hobbyists and professionals to select materials backed by verified mechanical properties.
Because material sciences and printing hardware evolve rapidly, our guide updates dynamically to reflect real-time developments. You can discover more consumer product analyses across our uncategorized reviews repository to stay informed on modern workshop tools.
Final Thoughts
Selecting the right photopolymer resin unlocks the full detail resolution of your LCD or DLP printing hardware. Pairing high-definition light engines with low-shrinkage formulations ensures crisp miniature features, smooth organic curves, and reliable dimensional fit.
For top-tier definition and reliable everyday printing, we recommend ANYCUBIC Upgraded 8K 3D Printer Resin as our best overall choice. Its high-definition grey finish accentuates microscopic surface contours while offering fast curing and excellent adhesion to build plates.
Budget-conscious makers seeking reliable general-purpose printing will appreciate ANYCUBIC 3D Printer Resin in black for its strong rigidity and dependable performance. Meanwhile, hobbyists crafting translucent gems or illuminated figures should opt for ANYCUBIC 3D Printer Resin in clear for its remarkable light transmission.
Check out our related resources on our home appliances hub to keep your workshop clean and organized. Investing in stable, quick-curing resins eliminates wasted print cycles and brings your 3D digital concepts to life with professional fidelity.
Frequently Asked Questions
What makes a formula one of the Best Resin 3D Printers consumables in 2026?
The premier resins combine rapid curing times with minimal shrinkage to preserve tight dimensional tolerances across detailed prints. They also maintain optimal fluid viscosity, allowing liquid photopolymer to flow smoothly underneath the build plate between every layer.
How do 405nm UV resins work with modern LCD 3D printers?
Liquid photopolymers contain reactive photoinitiators that absorb 405nm ultraviolet light emitted from printer arrays. When exposed to the light pattern, liquid monomers cross-link into solid polymer chains, building models slice by slice.
Why is high fluidity important when choosing resin for Best Resin 3D Printers in 2026?
High fluidity allows liquid resin to rush back over the release film quickly after the build plate retracts. This fast flow prevents vacuum bubbles, reduces peel forces, and allows shorter pause times between layer exposures.
How does resin shrinkage impact dimensional accuracy on mechanical parts?
When resin cures, molecular bonds pull closer together, creating linear contraction across the X, Y, and Z axes. Formulations with low shrinkage prevent wall warping, ensuring interlocking prototype components fit together precisely without secondary filing.
What is the ideal ambient temperature for curing resin in 2026?
Photopolymer resin performs best at room temperatures between twenty and twenty-five degrees Celsius. Colder environments thicken the liquid, which increases suction forces and can cause layer delamination or support failures.
How should I properly mix resin before starting a print?
You should vigorously shake the bottle for approximately sixty seconds before pouring liquid into the vat. Shaking ensures suspended pigment particles and chemical stabilizers mix thoroughly, preventing uneven coloration across your finished model.
Can I use 8K resin on standard 4K or 2K resin 3D printers?
Yes, high-definition 8K resin formulas are backward compatible with all 2K, 4K, 6K, and 12K LCD screens. The finer pigment milling in 8K resin helps capture crisp details regardless of your screen native pixel pitch.
How do I clean and wash parts printed with photopolymer resin?
Submerge finished parts in a bath of ninety-nine percent isopropyl alcohol or dedicated resin detergent for three to five minutes. Use a soft brush to dislodge unpolymerized liquid from recessed crevices before air drying and final UV curing.
Why is secondary UV post-curing necessary after washing?
The initial printing exposure only cures resin to approximately eighty percent green strength to prevent over-baking supports. Secondary curing under dedicated 405nm lamps completes polymer cross-linking, maximizing surface hardness and mechanical durability.
How do I safely dispose of contaminated alcohol and cured resin scrap?
Never pour contaminated cleaning alcohol or liquid resin down household plumbing drains. Expose waste wash alcohol to direct sunlight until dissolved resin solidifies, then filter out the cured plastic for safe solid waste disposal, as detailed in our health and family safety guides.


Write Your Review
No reviews yet. Be the first to share your experience!